
The Real Cost of Beverage Can Damage: How Beverage Manufacturers Maximize ROI with SmartSkin
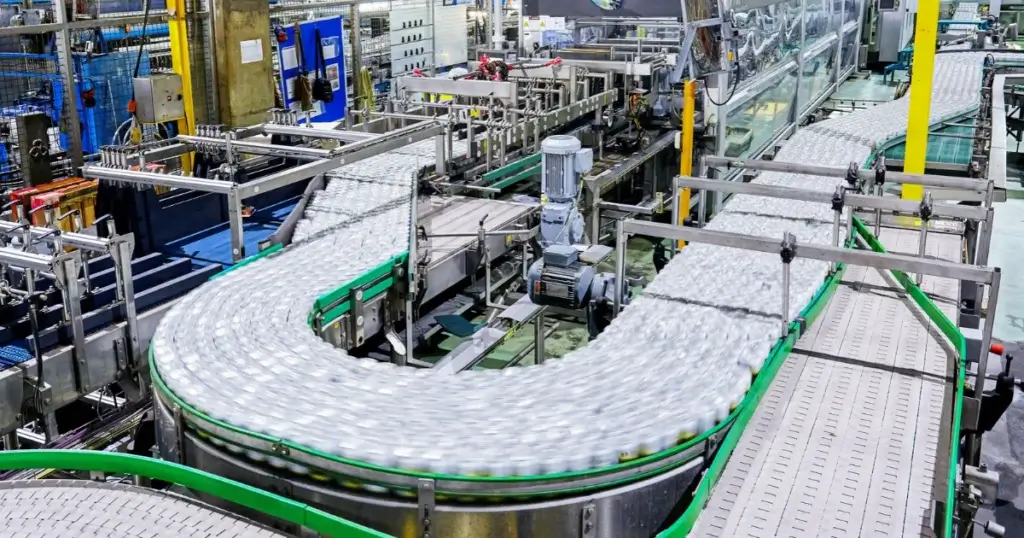
Beverage can damage on a high-speed production line rarely announces itself clearly. Industry research shows food and beverage manufacturers lose between $4,000 and $30,000 per hour during unplanned stoppages, and that figure does not include scrapped product, emergency repairs, or customer attrition. For one beverage manufacturer, those costs had reached $30,000 per day before SmartSkin was brought in to diagnose the problem.
This article looks at what real ROI means for beverage manufacturers using SmartSkin: not projected savings or estimated efficiency gains, but verified outcomes from documented production line scenarios. Two case studies illustrate how force data collected through Digital Container Twins and analyzed in Quantifeel™ software changes the economics of running a high-speed beverage line.
Key Takeaways
- Beverage can damage at 6.7% was costing one plant approximately $30,000 per day in product losses before SmartSkin intervention
- After targeted adjustments, damage was reduced to 0.0005%, a ratio of 1 damaged can per 180,000
- Persistent undiagnosed leakers drove QA pallet holds to 598 at one plant. After SmartSkin intervention, holds dropped to 137, a 77% reduction
- A lightweighting project delivered $600K in beverage can damage savings and avoided $1M in palletizer replacement costs within 3 months
- A format changeover causing leakers was resolved through a targeted 8% speed adjustment identified by SmartSkin, with no impact on overall line output
- In every case, root cause was identified without halting production or requiring OEM service intervention
How Beverage Can Damage Costs More Than Most Plants Realize
Beverage can damage is rarely a single-line problem. It compounds. A pressure imbalance that causes minor scuffing at one point on the line can accelerate structural failure further downstream. A leaker that goes undiagnosed for weeks drives customer complaints, QA holds, and production delays that accumulate far beyond the initial cost of the damaged unit. For most plants, the true cost of can damage only becomes visible after SmartSkin runs a diagnostic.
Equipment Misalignment: $30K in Daily Product Losses
For one beverage manufacturer experiencing severe beverage can damage at the heel of the can, the problem had escalated to line crashes and approximately $30,000 per day in product losses before SmartSkin was engaged. The plant initially suspected a single piece of equipment. What SmartSkin found was more complex, and more fixable.
Using Digital Container Twins running through the live production line and real-time pressure data captured in Quantifeel™ software, the SmartSkin team identified pressure peaks at two specific points: between the seamer and filler infeed, and at the head of the seamer. Those readings pinpointed the exact adjustments needed.
Results After SmartSkin Intervention
- Can damage reduced from 6.7% to 0.0005%
- Damage ratio dropped from 100 damaged cans per 180,000 to 1
- $30,000 in daily product losses eliminated
- Line crashes reduced significantly without any production halt
For the full technical breakdown of how the diagnosis was conducted and what adjustments were made, read the complete case study.
Undiagnosed Leakers: From 598 QA Holds to 137
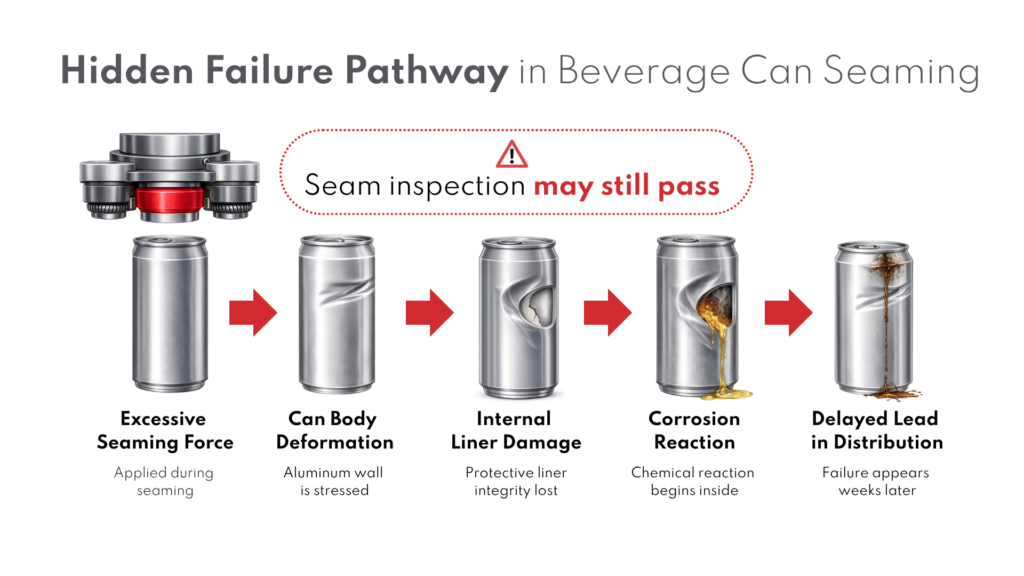
Leakers are among the most difficult beverage can damage problems to resolve without force data. The damage is often inconsistent, the root cause is rarely visible to the naked eye, and standard inspection methods cannot identify where on the line the pressure event is occurring.
For one plant, leakers had persisted consistently over a three to six month period with no diagnosis in sight. QA pallet holds had reached 598 and customer complaints were rising. Upon visual inspection, the same damage pattern appeared consistently at the mid wall and shoulder of affected cans.
Within 10 minutes of running SmartSkin through the filler seamer, we identified two distinct pressure events: excessive pressure at the filler infeed causing mid wall damage, and a secondary pressure spike at the scroll worm and starwheel transition point causing shoulder damage.
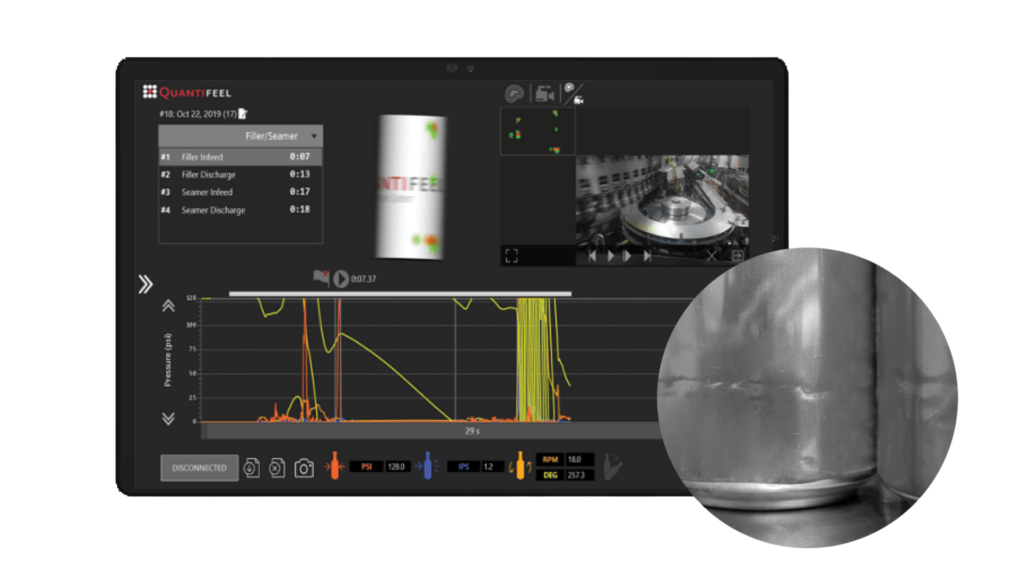
The maintenance team made targeted adjustments to timing and synchronization of the scroll worm, starwheel, and filler. When SmartSkin reviewed the data one year later, the adverse forces had been fully eliminated.
Results After SmartSkin Intervention
- QA pallet holds reduced from 598 to 137, a 77% reduction
- Leakers and shoulder dents fully eliminated
- Root cause confirmed within a single diagnostic session
- Results sustained and verified one year later
For the full case study, read the complete story.
Lightweighting: When Beverage Can Damage Gets Worse with Lighter Cans
Lightweighting is one of the most commercially compelling initiatives in beverage manufacturing today. Thinner, lighter cans reduce material costs and support sustainability targets. But they also make beverage can damage far more likely. Pressure levels that a standard can absorbed without issue can crush, dent, or deform a lightweight can at the same line settings.
For one plant looking to transition to lighter cans while maintaining existing machine centers and conveyors, the initial assessment was discouraging. The plant was advised that its line in its current condition could not support the switch, and that the palletizer would need to be replaced at an approximate cost of $1M.
SmartSkin was called in before the lightweighting project began to assess areas of inefficiency across the full line. We identified multiple hotspots, particularly feeding into the SMI Packer, where pressure was maxing and causing damage to standard cans. Those same pressure levels would be significantly more destructive to lightweight cans.
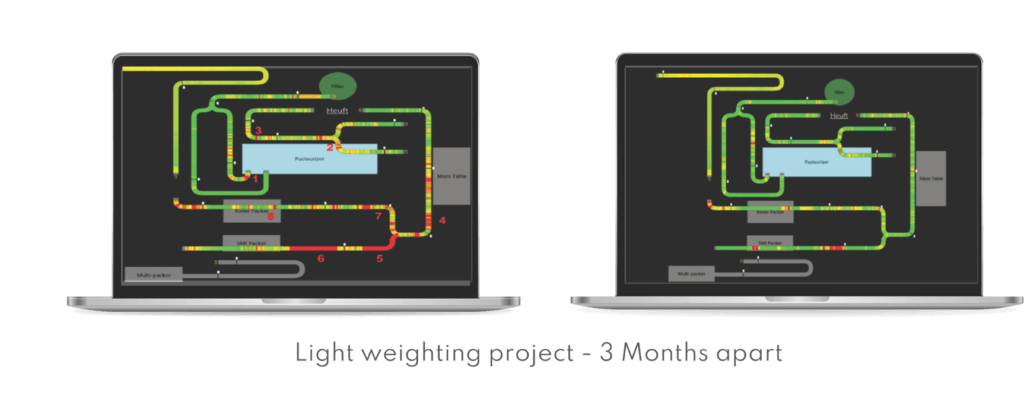
Within 3 months, using only internal resources, the plant addressed every flagged area. Conveyor speeds were modified, PLCs corrected, proxy sensors repositioned, and guard rail alignment improved. The palletizer issue, initially deemed irreparable, was identified precisely enough to be fixed without replacement.
The results:
- Major can damage fully eliminated
- Minor damage significantly reduced
- Line successfully adapted for lightweight cans within 3 months
- $600K saved from can damage reduction
- $1M avoided by retaining the existing palletizer
- Total documented impact: $1.6M
For the full case study including before and after pressure mapping, read the complete story.
Format Changeovers: When a New Can Size Triggers Beverage Can Damage
Changeovers are one of the most disruptive triggers of beverage can damage on a high-speed production line. A line that runs perfectly on one can format can develop entirely new damage patterns the moment a different format is introduced. The variables shift, the tolerances tighten, and problems that were invisible before suddenly appear at speed.
For one beverage manufacturer running SmartSkin across three of their production lines, a new can format introduced to one line triggered unexpected can damage and leakers on equipment that had never previously given them issues. The plant needed to identify whether the problem was the equipment, the format, or the interaction between the two.
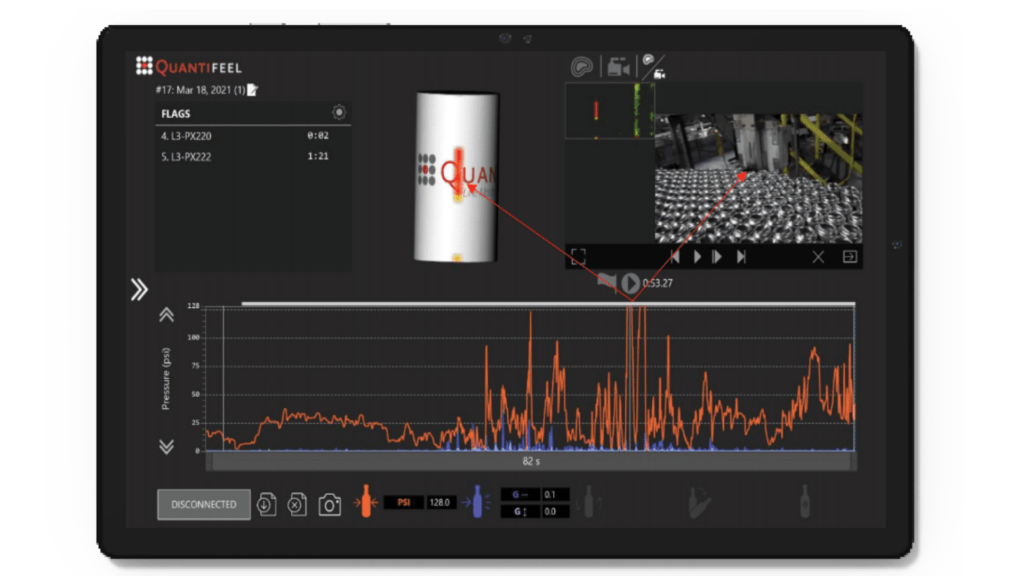
Using Digital Container Twins in the new format and pressure data captured in Quantifeel™ software, SmartSkin identified repeatable pressure spikes occurring at a specific point in the conveyor. The root cause was not a mechanical failure. It was a geometry mismatch between the new can diameter and the existing conveyor configuration at the s-curve.
The fix was precise and immediate:
- A targeted 8% speed reduction leading up to the s-curve eliminated the pressure causing sidewall damage
- Leakers were eliminated entirely following each subsequent format changeover
- No impact on overall line speed or production output
For the full case study including pressure profile data, read the complete story.
The Bottom Line
Beverage manufacturers do not have the luxury of tolerating unexplained beverage can damage, recurring leakers, or line crashes that eat into daily output. The cost accumulates fast, and the root cause is rarely where the symptoms first appear.
What all four cases documented here share is not just a positive outcome. They share a diagnostic process that replaced guesswork with precision. Digital Container Twins running through live production lines, capturing real-time force data in Quantifeel™ software, identified the exact source of damage in every scenario without halting production, without waiting for an OEM service call, and without weeks of trial-and-error adjustments.
The financial impact goes beyond product saved and crashes avoided. At one plant, integrating SmartSkin into daily operations eliminated $300K per year in product waste from leakers and reduced $350K in annual OEM service costs, resources that were immediately reallocated to other priorities.
That is what ROI looks like for beverage manufacturers using SmartSkin. Not a projected estimate. A documented outcome on a real line, measured in product saved, crashes avoided, and daily losses eliminated.
If you want to understand what that looks like for your specific line configuration, we can build a custom ROI calculation based on your current damage rates and production volumes.
Frequently Asked Questions
How quickly can SmartSkin identify the root cause of can damage on a beverage line?
In most cases, SmartSkin Digital Container Twins can be run through a live production line and generate actionable pressure and force data within a single production session. Our solutions display results in real time, meaning your team can identify damage sources and begin implementing adjustments the same day without halting production.
Does SmartSkin require a production shutdown to run diagnostics?
No. Digital Container Twins are designed to run through your live line under normal production conditions. There is no need to stop the line, remove equipment, or schedule downtime for a diagnostic run. This is one of the key operational advantages SmartSkin provides over traditional diagnostic approaches.
Can SmartSkin help with beverage can damage that only appears after a format changeover?
Yes. Format changeovers introduce new can geometries that interact differently with existing conveyor configurations, guide rails, and infeed timing. SmartSkin Digital Container Twins can be run in the new format immediately following a changeover to capture pressure and force data specific to that configuration, identifying damage sources that would otherwise require extensive manual investigation.
What types of beverage lines does SmartSkin work with?
SmartSkin Digital Container Twins are compatible with high-speed canning lines across a range of formats and production environments, including aluminum can lines running multiple SKUs and formats. The technology has been deployed by leading global beverage manufacturers including Coca-Cola, Pepsi, Heineken, and Carlsberg.
How do beverage manufacturers calculate ROI from SmartSkin?
ROI from resolving beverage can damage varies by plant, line configuration, and damage profile. The most direct measure is daily product loss eliminated after SmartSkin intervention. For manufacturers experiencing significant damage rates, the payback period is typically short because the cost of unresolved damage accumulates rapidly. SmartSkin can provide a custom ROI calculation based on your current damage rates, production volumes, and line configuration. Contact us to get started.