
Factory Acceptance Testing for Pharma Fill-Finish
When new fill-finish equipment arrives at your facility, the pressure to get it qualified and into production is real. Timelines are tight, budgets are fixed, and every delay has a cost. Factory acceptance testing is the stage where that pressure meets its first real test, and where the decisions you make have consequences that follow the equipment for its entire operational life.
A well-executed FAT catches design flaws, integration gaps, and performance inconsistencies before they become production problems. A poorly executed one passes those same issues downstream, where they are far more expensive to fix and far more likely to trigger regulatory scrutiny.
This guide covers what factory acceptance testing looks like in pharmaceutical fill-finish operations, how it connects to site acceptance testing, and how teams are using real-time force data to build stronger qualification baselines from day one.

Key Takeaways
- Factory acceptance testing is the first documented opportunity in the qualification lifecycle [3] to verify that fill-finish equipment meets its design specifications in a GMP context.
- Design errors caught at FAT cost significantly less to resolve than those identified after installation, commissioning, or commercial production.
- A comprehensive pharma FAT includes static checks (safety, GMP construction, utilities, documentation) and dynamic checks (rate verification, container quality, capper head consistency, induced failure testing).
- Standard dynamic checks confirm that equipment runs at speed but do not capture per-head mechanical force variation in capping and crimping stations.
- Force data collected during FAT establishes a mechanical baseline that supports SAT comparison, container closure integrity strategy, and process centerlining throughout the equipment lifecycle.
- A well-executed FAT with complete documentation reduces SAT deviation risk, compresses go-live timelines, and strengthens your overall qualification package.
Why Factory Acceptance Testing Matters in Pharma
In pharmaceutical manufacturing, factory acceptance testing is rarely optional. For fill-finish equipment, it is the first documented evidence that a piece of equipment meets its user requirements before it ever enters a GMP environment. Even on projects where the full IQ/OQ/PQ qualification sequence is streamlined, FAT is typically retained because it addresses the two risks that matter most at this stage: functionality and budget. Catching a design gap or a performance shortfall at the supplier's facility costs a fraction of what the same issue costs after installation. For regulated manufacturers, it also creates the paper trail that supports everything that follows in the qualification lifecycle.
The further a design error travels through the qualification process, the more expensive it becomes to fix. A defect caught at the supplier's facility during FAT can typically be resolved within the same visit. The same defect discovered after installation requires travel, downtime, potential requalification, and in some cases a regulatory deviation report. For fill-finish lines handling sterile drug products, the stakes are higher still. Any equipment failure that reaches commercial production carries patient safety implications that no cost curve can fully capture. A rigorous FAT is the most cost-effective intervention point in the entire equipment lifecycle.

Factory acceptance testing does not exist in isolation. It is the first step in a qualification sequence that runs through SAT, installation qualification (IQ), operational qualification (OQ), and performance qualification (PQ). What happens at FAT directly shapes the efficiency of every phase that follows.
Operator and maintenance technician training typically begins during FAT, giving teams direct exposure to the equipment before it arrives on site. Integration requirements with adjacent line equipment, including conveyor heights, star wheel tolerances, and reject system interfaces, are confirmed at this stage rather than discovered during SAT. Documentation packages including OEM manuals, spare parts lists, and control programming are reviewed and any gaps flagged before shipment.
For fill-finish operations, this early alignment between supplier and manufacturer is particularly valuable. Lines handling sterile drug products have limited tolerance for post-installation surprises. A thorough FAT compresses the risk window and gives qualification teams a reliable baseline to build on.

A fill-finish facility faced challenges when adapting existing equipment to handle multiple primary packaging formats.
By implementing SmartSkin’s technology, the facility identified defects early, reduced downtime, and improved line performance.
Developing a FAT Test Plan for Fill-Finish Equipment
A FAT test plan for fill-finish equipment starts well before anyone sets foot on the supplier's floor. It is built from three inputs: the User Requirements Specification (URS), the equipment design specification [3], and the agreed key performance indicators (KPIs) for the line. When all three are aligned, the test plan gives every party involved, including the supplier, the manufacturer's engineering team, and quality assurance, a shared reference for what acceptable performance looks like. The acceptance testing FAT process procedure should be reviewed and signed off by both the manufacturer's quality team and the equipment supplier before the FAT date is confirmed.
For fill-finish equipment, the test plan should explicitly define acceptance criteria for the parameters that matter most in a GMP environment. That includes fill accuracy, capper or crimper head consistency, container handling forces, reject system performance, and alarm response behavior. Using "Acceptable" and "Not Acceptable" classifications rather than strict pass/fail gives teams the flexibility to document deviations without halting the entire FAT for minor non-conformances.
Documentation requirements should be defined upfront. Every inspection result needs a dedicated space in the protocol, along with room for unforeseen observations. A signature page for each completed section is not a formality; it is the evidence trail that supports milestone payments, SAT planning, and ultimately your IQ/OQ/PQ documentation package.
For complex fill-finish lines, a Pre-FAT visit is worth scheduling. It confirms the equipment is ready for formal testing before a large cross-functional team travels to the supplier's facility, avoiding the cost and frustration of showing up to an incomplete machine build.
Pre-FAT Planning: Confirming Readiness Before the Visit
Before the formal FAT begins, a Pre-FAT visit is worth scheduling for complex fill-finish equipment. Its purpose is straightforward: confirm the machine is built, functional, and ready for formal testing before a cross-functional team travels to the supplier's facility. A failed Pre-FAT costs one person a trip. A failed FAT costs the entire team time, travel, and schedule delays that ripple through the qualification timeline.
During the Pre-FAT, the supplier should demonstrate that all major systems are operational, documentation packages are in progress, and any open punch list items from the design review have been closed or formally acknowledged. For fill-finish equipment specifically, this is also a good opportunity to confirm that the container formats being tested at FAT match the actual production specifications.
FAT Execution: What Happens on the Day
On the day of FAT, the team assembles at the supplier's facility with the approved test plan in hand. Each team member should have a clearly defined role, whether that is executing specific test protocols, documenting results, or making acceptance decisions on behalf of the manufacturer. For fill-finish FATs, this typically means representation from engineering, quality assurance, and operations. A testing FAT process procedure checklist should be in the hands of every team member before testing begins, with roles and responsibilities clearly assigned against each item.
Clear documentation practices need to be established before testing begins. Some organizations have strict protocols around how corrections are made in test records, including the color of pens used and how errors are struck through. These are not bureaucratic details. In a GMP context, the integrity of FAT records directly supports the validity of your qualification documentation downstream.
Establishing a shared understanding of acceptance criteria before testing starts is equally important. "Acceptable" and "Not Acceptable" classifications give teams a consistent framework for making decisions in the moment without stopping the FAT every time a minor deviation is observed.
What FAT Checks Cover in Pharmaceutical Manufacturing
FAT checks can be categorized into two groups: static checks and dynamic checks [2].
Static Checks
Static checks are completed while the equipment is not running. In a pharmaceutical context, these go beyond mechanical verification and extend into GMP compliance requirements.
Safety: Verify that all safety features, emergency stop devices, and interlocks meet federal, local, and corporate standards. Confirm that energy within the system can be fully isolated and locked out before maintenance access is required.
Layout: Confirm that the equipment's physical layout matches approved drawings and integrates correctly with adjacent line equipment. For fill-finish lines, this includes conveyor heights, star wheel tolerances, and the positioning of rejection systems relative to fill and capping stations.
GMP Construction: Inspect materials of construction for all product-contact surfaces. Confirm surface finishes meet cleanability requirements and that the equipment design supports routine cleaning and sanitization without dead legs or inaccessible areas.
Utilities: Confirm provisions for all required utilities including compressed air, electrical supply, water for injection (WFI), and nitrogen where applicable. Verify parameters including pressure ratings, consumption values, voltage, and fuse specifications against project requirements.
Documentation: Review the progress of all documentation packages including OEM manuals, spare parts lists, operating manuals, and control programming. Flag any gaps before shipment. Incomplete documentation at FAT becomes a SAT deviation.
Dynamic Checks
Dynamic checks are completed while the equipment is running at production conditions. For fill-finish equipment, these checks go beyond confirming that the machine runs at speed.
Rate Verification: Confirm the equipment operates at required speeds for a sustained period without faults. Test at both nominal and peak speeds to establish the full operating envelope.
Quality Checks: Verify that the equipment does not introduce damage or quality defects to the container. For fill-finish lines, this includes visual inspection of containers post-capping or post-crimping, as well as force profiling to confirm that mechanical loads applied to each container fall within qualified parameters.
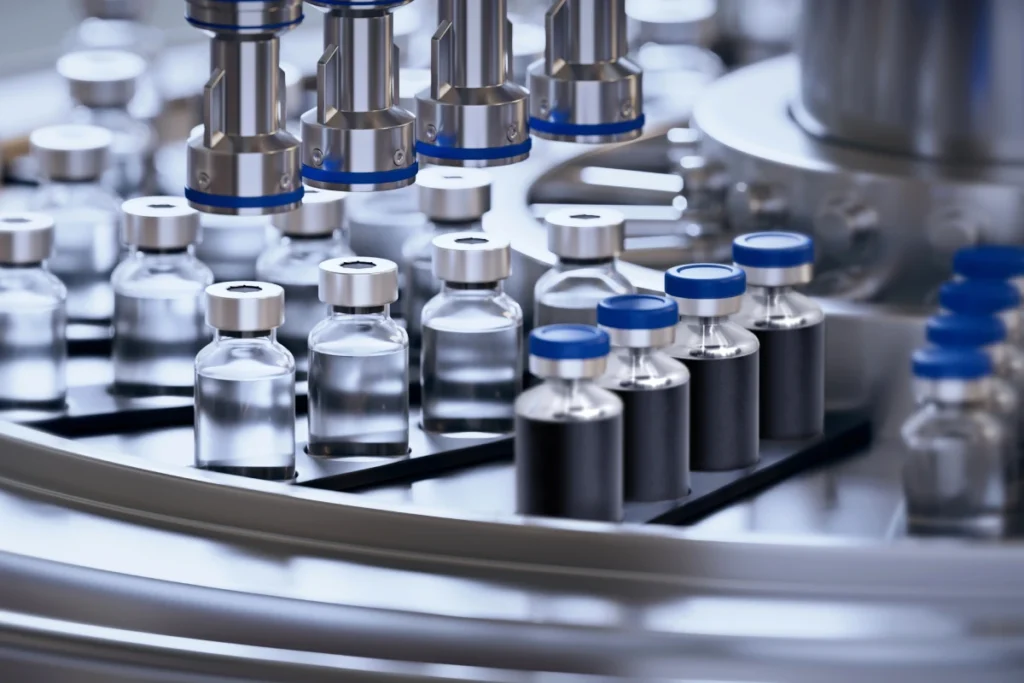
Capper and Crimper Head Consistency: Each head on a multi-head capper or crimper applies force independently. Dynamic checks should confirm that force output is consistent across all heads. Head-to-head variation that passes visual inspection can still produce containers with inconsistent seal performance. Real-time force data captured during FAT establishes the baseline against which future head performance can be compared.
Functional Checks: Verify that the equipment performs its intended functions correctly under different operating conditions. This includes start-up sequences, container handling behavior, jogging, homing functions, and reject system activation.
Induced Failure Testing: Evaluate the equipment's ability to detect and recover from typical fault conditions. Start the equipment under simulated production conditions, introduce fault conditions intentionally, observe HMI response and error messaging, demonstrate recovery to normal running, and document each sequence in full. Repeat for all relevant fault conditions.
How SmartSkin Supports FAT/SAT in Fill-Finish Operations
Standard FAT dynamic checks confirm that fill-finish equipment runs at speed, handles containers without visible damage, and responds correctly to fault conditions. What they do not capture is the mechanical force each container experiences as it moves through capping or crimping stations, and whether that force is consistent from one head to the next.
Head-to-head variation in capping and crimping equipment is one of the most common sources of container closure integrity risk in fill-finish operations. A capper running six heads may show no visible quality defects at FAT while two of those heads are applying forces outside the qualified range. That variation does not disappear after installation. It follows the equipment into production, where it becomes an intermittent quality problem that is difficult to trace back to its root cause.
SmartSkin's solutions give fill-finish teams a way to capture that data during FAT. By running through the line at full production speed, SmartSkin measures the forces applied to each container at every capping or crimping head in real time. The result is a head-by-head mechanical baseline, documented at the point of qualification, that gives teams an objective reference for evaluating equipment performance throughout its operational life.
That baseline has value beyond FAT. When the same measurement is repeated at SAT, any shift in force profile between the supplier's facility and the installed line becomes immediately visible. Teams can confirm that transport and installation have not affected equipment performance, or identify and resolve issues before the qualification package is closed.
For manufacturers building a container closure integrity strategy [1], force data collected at FAT and SAT is the earliest layer of evidence that the capping or crimping process is operating within defined parameters. It supports quality by design principles [4], strengthens process centerlining, and gives quality teams the documentation they need to demonstrate control from day one.
In Conclusion: The Significance of Factory Acceptance Testing
Factory acceptance testing is not a box to check before equipment ships. For fill-finish operations handling sterile drug products, it is the clearest opportunity in the entire qualification lifecycle to establish that equipment performs as intended, document that performance in a way that satisfies regulatory expectations [5], and build a baseline that supports every qualification phase that follows. When the factory acceptance testing FAT process includes real-time force data alongside standard functional and visual checks, qualification teams leave the supplier's facility with a stronger, more complete evidence package.
The difference between a FAT that merely passes and one that genuinely de-risks the qualification program comes down to how thoroughly it is planned, how rigorously it is executed, and what data it produces. Visual inspection and functional checks confirm that equipment runs. Force data confirms that it runs correctly, consistently, and within the parameters that protect container closure integrity.
Teams that conduct thorough factory acceptance tests arrive at SAT with fewer surprises., close their documentation packages faster, and enter commercial production with greater confidence in their line performance.
Frequently Asked Questions
References
[1] European Commission, Annex 1 to the EU Guidelines for Good Manufacturing Practice: Manufacture of Sterile Medicinal Products, EudraLex Volume 4, 2022, https://health.ec.europa.eu/medicinal-products/eudralex/eudralex-volume-4_en
[2] ASTM International, ASTM E2500: Standard Guide for Specification, Design, and Verification of Pharmaceutical and Biopharmaceutical Manufacturing Systems and Equipment, ASTM, 2013, https://www.astm.org/e2500-07r13.html
[3] ISPE, Good Practice Guide: Equipment Qualification, ISPE, 2019, https://ispe.org/publications/guidance-documents/good-practice-guide-equipment-qualification
[4] ICH, Q8(R2): Pharmaceutical Development, ICH, 2009, https://www.ich.org/page/quality-guidelines
[5] FDA, Pharmaceutical CGMPs for the 21st Century: A Risk-Based Approach, FDA, 2004, https://www.fda.gov/media/77391/download